2013
Tianjin Zhongtian Heavy Industry Group Co., Ltd. was officially established. Rooted in the trade of industrial chemical raw materials and supply chain services, the company embarked on a path of specialized development.
about us
Deeply Rooted in Fine Chemicals • Focused on Green New Energy
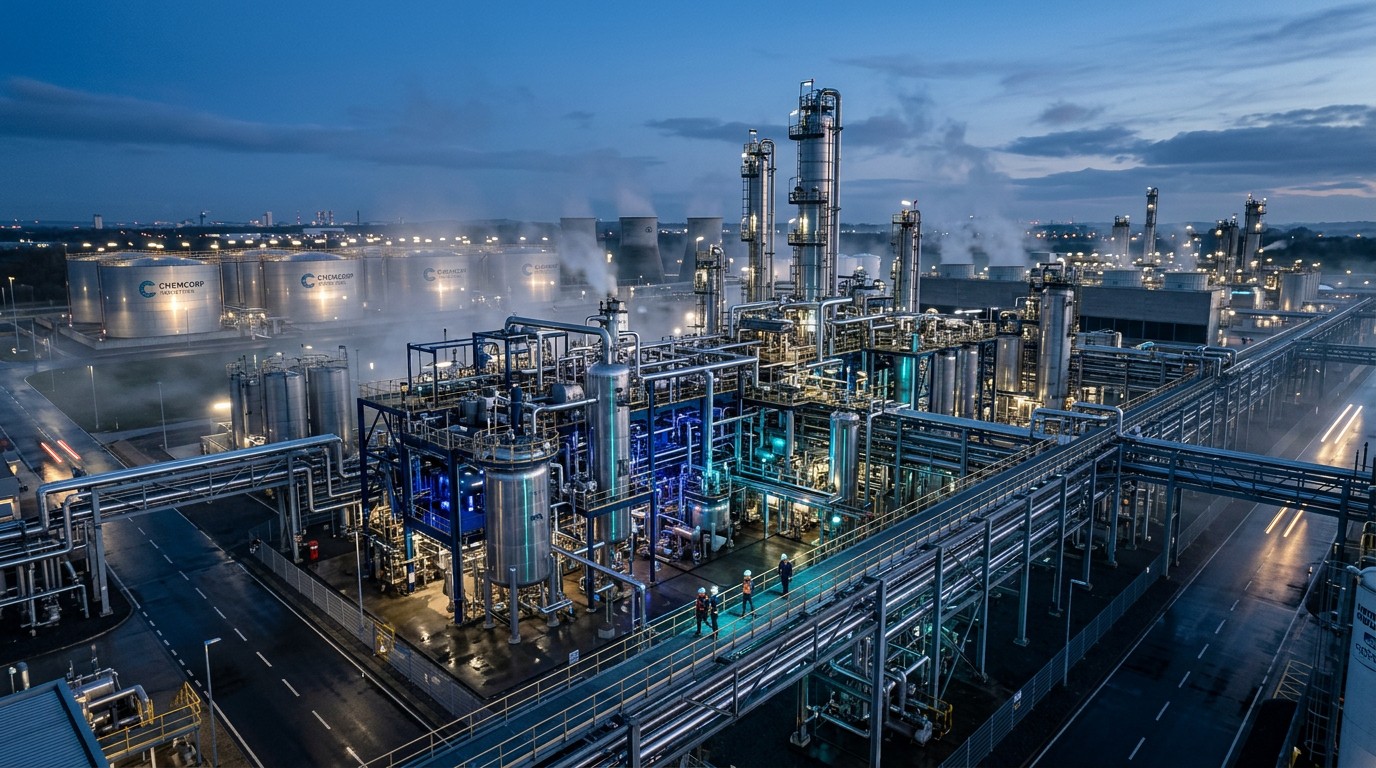
Tianjin Zhongtian Heavy Industry Group Co., Ltd. specializes in the R&D, supply, and global distribution of high-purity industrial chemical raw materials. We are dedicated to providing stable, reliable, and competitive raw material solutions to industries such as chemical manufacturing, detergents and personal care, water treatment, food processing, textile printing and dyeing, construction materials, and plastics processing.
Underpinned by a rigorous quality management system, the company continuously integrates premium production resources and international supply chain capabilities. Our core product portfolio includes anhydrous citric acid, linear alkylbenzene sulfonic acid (LABSA), sorbitan fatty acid esters, caustic soda, polyvinyl chloride (PVC), and borax pentahydrate. We maintain end-to-end control—spanning raw material selection, production coordination, quality testing, warehousing, and cross-border logistics—to ensure that product purity, batch consistency, and delivery efficiency meet the specific application requirements of diverse markets.
Backed by a professional international trade team, a robust supply chain network, and a responsive customer service system, the company has established long-term partnerships with over 800 corporate clients across more than 80 countries and regions. Beyond supplying standardized products, we offer tailored procurement and logistics support customized to each client's specific industry applications, specifications, packaging preferences, and delivery schedules.
0
+
Years Industry Experience
0
+
Global Clients Served
280
+
Dedicated Professionals
500
+
Product Series
Company History